Industrial Intelligence: The Next Growth Engine for Manufacturing
The essence of industrial intelligence is transforming knowledge scattered in documents and veteran employees' minds into reusable, transferable digital assets.
The article points out that the core of industrial intelligence is not piling up sensors or deploying large models, but explicating the tacit knowledge long deposited in documents and veteran employees' experience in manufacturing into reusable, transferable organizational assets. Traditional automation systems (PLC, SCADA, MES, ERP) excel at deterministic rules but struggle to capture fuzzy associations such as material behavior and shift history, leaving a blank zone for knowledge modeling. The entry scenarios for industrial intelligence focus on three directions: changeover and restart assistance, knowledge transfer, and anomaly tracing. Implementation barriers lie not only in data silos but also in organizational resistance and the high cost of knowledge modeling. The next round of growth opportunities in manufacturing belongs to pioneers who systematically advance knowledge assetization; decision-makers should prioritize selecting appropriate entry scenarios.
Every leap in manufacturing is accompanied by a shift in the form of knowledge. As digital transformation enters deep waters, a concept that is repeatedly mentioned but rarely truly defined has surfaced—industrial intelligence.
What Is Industrial Intelligence: More Than Data, It's the Explicitation of Knowledge
The source material offers an intriguing definition: every manufacturer possesses its own industrial intelligence, part of which is documented and part of which resides in the knowledge of experienced workers. This statement pierces a long-standing structural contradiction in manufacturing—the most core competitiveness of an enterprise is often deposited in the carriers that are hardest to replicate.
Imagine an experienced operator preparing to restart a production line after a changeover. Machine parameters are certainly important, but equally critical are: the behavioral characteristics of this material under specific conditions, what happened during the previous shift, and how a seemingly minor anomaly escalates into a systemic risk under specific circumstances. A considerable proportion of these judgment bases do not appear in any SOP, but exist in the operator's intuition and experience as tacit knowledge.
The true value of industrial intelligence lies not in piling up sensors or deploying large models, but in transforming this scattered, implicit knowledge into reusable, transferable assets. This is both a technical problem and an organizational problem.
Tacit Knowledge was proposed by philosopher Michael Polanyi, referring to knowledge that is difficult to fully express through language, text, or symbol systems, such as a craftsman's touch or an operator's intuitive judgment. In contrast, Explicit Knowledge is codifiable and documentable. In manufacturing, SOPs and process documents belong to explicit knowledge, while "judging equipment status by listening to sounds" and "adjusting parameters by feel" belong to tacit knowledge. Polanyi's classic proposition "We know more than we can tell" precisely captures this dilemma. The core challenge of industrial intelligence is precisely to use data collection, pattern recognition, and knowledge engineering to partially transform tacit knowledge into computable, communicable explicit assets—a process known in knowledge management as Externalization.
Where Is the Disconnect Between Automation and Intelligence?
Over the past decades, manufacturing automation investments have mainly focused on two directions: first, control-layer automation represented by PLC and SCADA, which solves the problem of "machines executing according to instructions"; second, information-layer integration represented by MES and ERP, which solves the problem of "data being recorded and circulated." Together they built the digital skeleton of the factory, yet left a significant blank zone—the capture and modeling of unstructured experience.
Traditional rule engines excel at handling deterministic logic such as "if temperature exceeds threshold, trigger alarm," but are often powerless when faced with fuzzy associations like "this material's flowability decreases when humidity is high, causing the first few products after changeover to be prone to insufficient filling." This is precisely the watershed between industrial intelligence and traditional automation systems: the former attempts to understand context and causality, while the latter only executes preset rules.
PLC (Programmable Logic Controller) and SCADA (Supervisory Control and Data Acquisition) are the two cornerstones of the industrial control layer. PLC is responsible for executing deterministic instructions such as logic control and sequence control, directly driving machine equipment; SCADA collects on-site data at the host computer level and provides human-machine interfaces and alarm management. Together they constitute the "nerve endings" of the modern factory. MES (Manufacturing Execution System) sits between the control layer and ERP, responsible for production scheduling, process management, and quality traceability; ERP (Enterprise Resource Planning) coordinates business resources such as finance, procurement, and inventory. Although this layered architecture (ISA-95 standard) achieves data connectivity from the shop floor to management, its original design intent is to handle structured, deterministic information flows and lacks modeling capability for experiential, contextual knowledge—this is precisely the technical root of the "disconnect" described in the text.
Three Key Dimensions of Industrial Intelligence Implementation
Starting from the clues in the source material, three core scenarios where industrial intelligence plays a role can be identified.
Changeover and Restart: Assistance for High-Risk Decisions
Changeover is a high-incidence segment for on-site accidents and quality fluctuations. Operators need to make judgments in a short time by integrating multi-source information such as equipment status, material characteristics, and shift history. If an industrial intelligence system can present this information in a contextualized manner—for example, prompting based on historical data that "this material is recommended to extend preheating time under current environmental conditions"—it can significantly reduce dependence on individual experience.
Changeover refers to a series of adjustments to equipment parameters, molds, material supply, etc., when a production line switches from producing one product to another. Changeover is a key efficiency bottleneck in lean production (as targeted by SMED rapid changeover methodology) and also a high-incidence point for quality fluctuations, because equipment status, material batches, and environmental conditions undergo sudden changes at this moment, and historical steady-state data no longer applies. The first batch of products after changeover often requires additional inspection, and operators need to comprehensively judge multidimensional information such as equipment thermal state, new material flowability, and mold wear degree, with decision complexity far higher than steady-state production. This is precisely a typical scenario where industrial intelligence assists decision-making with contextualized knowledge.
Knowledge Transfer: Migration from People to Systems
The knowledge loss brought by the retirement of senior employees is a real challenge faced by many manufacturing enterprises. Industrial intelligence offers a new path: through analysis of operation records, exception handling logs, and even on-site communication content, implicit decision patterns are distilled into a queryable knowledge base. This is not simple document archiving, but letting the system learn to "think like a master craftsman".
Anomaly Tracing: From Symptom to Root Cause
When quality deviations occur on the production line, traditional methods rely on engineers' personal experience to investigate item by item. Industrial intelligence can quickly narrow the problem scope through correlation analysis of multidimensional historical data. The "seemingly minor anomalies" mentioned in the source material are precisely the key—the early signals of many major failures are extremely weak, and only an intelligent system that is online at all times can capture such signals and establish causal chains.
Implementation Challenges: The Real Obstacles Beyond Data
Advancing industrial intelligence is far from being as simple as technical deployment. Data on the manufacturing floor is often scattered across systems of different eras, different vendors, and different protocols, forming de facto data silos. More troublesome is the resistance at the organizational level: frontline operators worry about being replaced by systems, middle managers worry that their value will decline after their experience is "drained," and collaboration barriers between IT and OT teams often cause projects to stall.
Another easily underestimated problem is the cost of knowledge modeling. Explicating tacit knowledge requires deep collaboration between domain experts and data scientists, with long cycles and large investments, and the results are difficult to quantify in the short term. This plunges many enterprises into the dilemma of "being unable to calculate the input-output account" at the pilot stage.
Conclusion: Growth Opportunities Belong to Pioneers of "Knowledge Assetization"
The next growth opportunity for manufacturing lies not in simply adding automation equipment or deploying more sensors, but in systematically transforming industrial intelligence—the knowledge scattered in documents and minds—into reusable, evolvable digital assets. The judgment of the source material is accurate: every manufacturer possesses its own industrial intelligence; the difference is that some enterprises are letting it settle down, while others allow it to dissipate with personnel turnover.
For decision-makers, the real question is not "whether to do industrial intelligence," but "from which scenario to start, so that the organization can feel the value of knowledge assetization within a visible cycle." Changeover assistance, knowledge transfer, and anomaly tracing—these three directions may provide starting points worthy of priority consideration.
Related articles

Overmind: An Open-Source Continual Learning Platform That Turns Production Traces into Custom Models
Overmind is an open-source continual learning platform launched on Product Hunt for AI teams. It turns production traces into team-owned custom models, covering training, benchmarking, and model serving.
Nuvio 5.0: Handing Financial Back Office to AI Agents
Nuvio 5.0 launches on Product Hunt to hand financial admin to AI agents—automated invoicing, expenses, and reconciliation—with ChatGPT, Claude, or custom agent access, plus new bookkeeping and tax services.
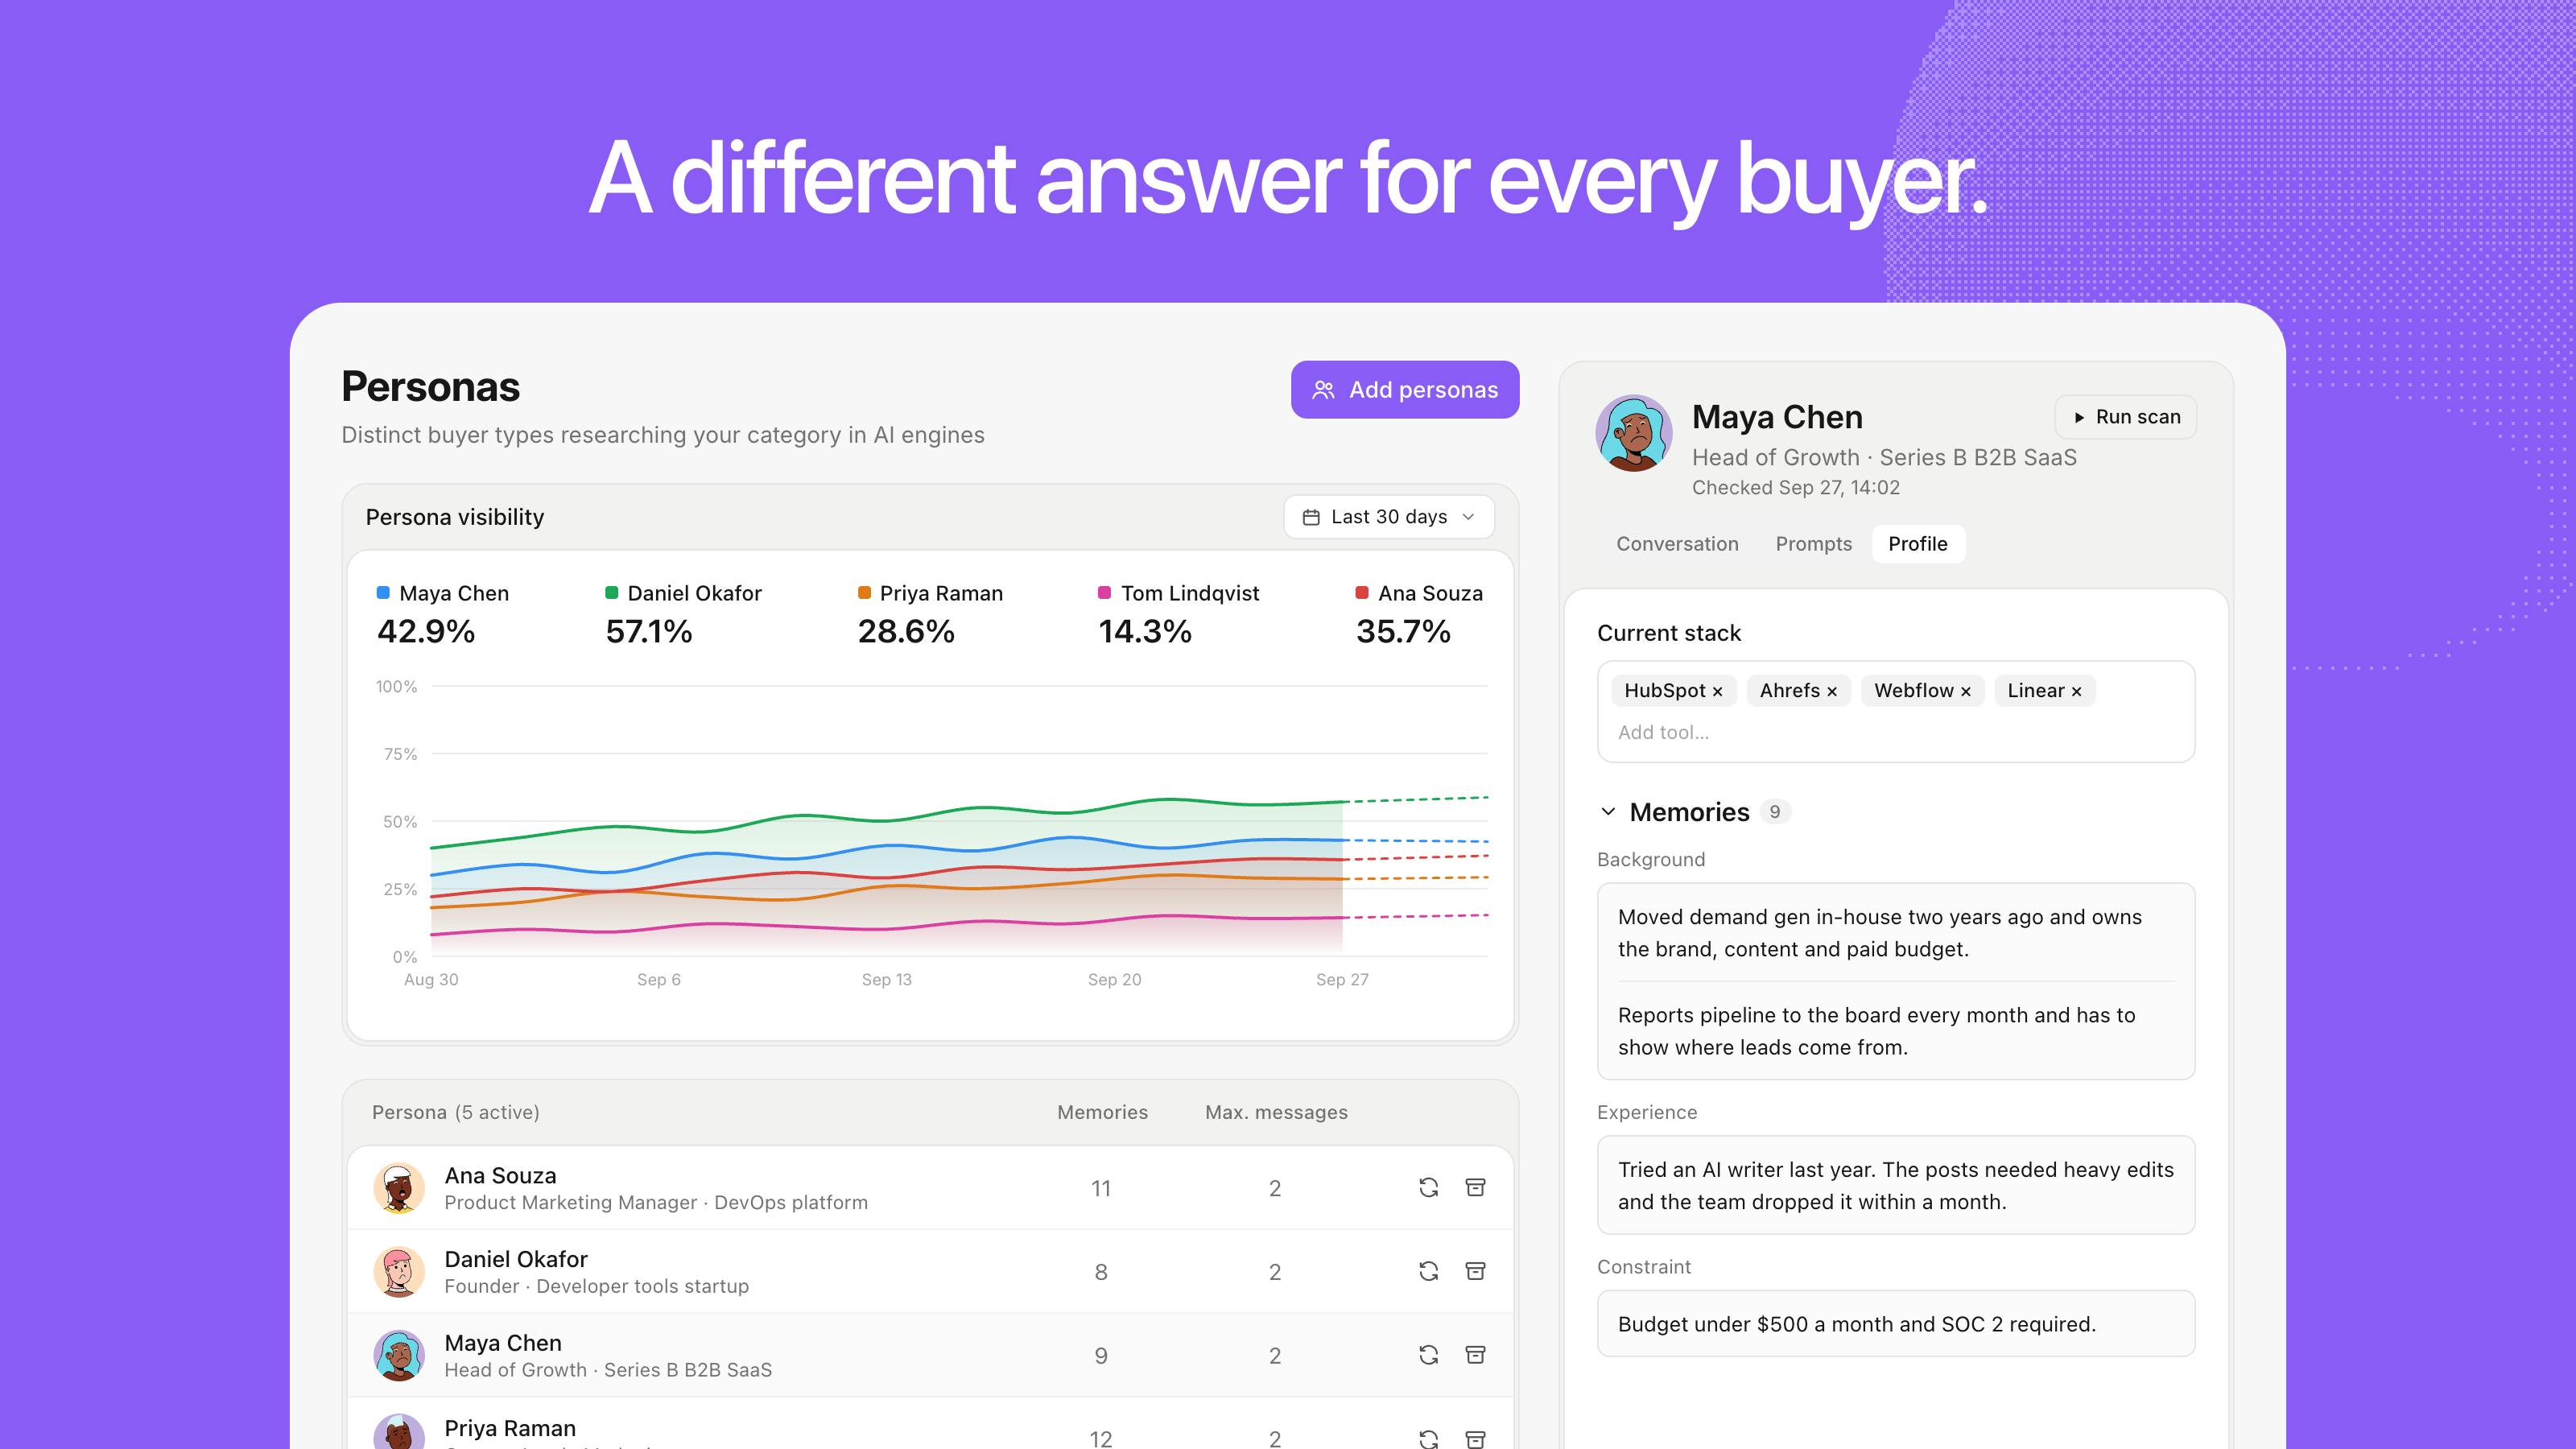
Notra: The GEO Tool That Helps Your Brand Stand Out in AI Search
Notra is a GEO tool that simulates buyer questions to ChatGPT, Claude, and Gemini to check brand visibility in AI search and provide optimization tips, helping marketers boost exposure in the generative AI era.